1-805-484-2992
Quotes - Engineering - SalesThe most heat transfer per square foot of floor
A sanitary plate and frame exchanger hangs a stack of thin, pressed stainless plates between a fixed and a movable frame plate and clamps them with tie bolts. Gaskets on each plate seal the edges and direct product and utility into alternating channels, so the two fluids run in true counterflow across the corrugated surface. Turbulence starts at low velocity, heat transfer coefficients run several times those of a tube, and the approach temperature can be brought to 2 or 3 F. Add a third fluid section and the same frame does regeneration, heating and cooling in one unit, which is why nearly every HTST pasteurizer is a plate exchanger.
Plates and gaskets
- 304L or 316L plates, 0.5 to 51 sq ft each
- Chevron, free-flow and wide-gap pressings
- Clip-on or glued gaskets in EPDM, nitrile, FKM
- Vented double gasket at every port keeps fluids apart
- Plate finish smooth as pressed; 32 Ra or electropolished on request
Frames and connections
- 304 stainless clad or solid stainless frames
- Tri-clamp studded ports 1" to 6", larger with sanitary flanges
- Stainless shrouds over the pack where required
- Tie bolts and bars in stainless, plate pack opens on the bars
- Multi-section frames with connection plates for regeneration
Ratings and codes
- 150 psig design typical, higher with heavier frames
- Gasket temperature limits generally 250 F for EPDM, higher for FKM
- 3-A plate exchanger standard where specified
- ASME U-stamp on the frame when required
- PED and CRN on request
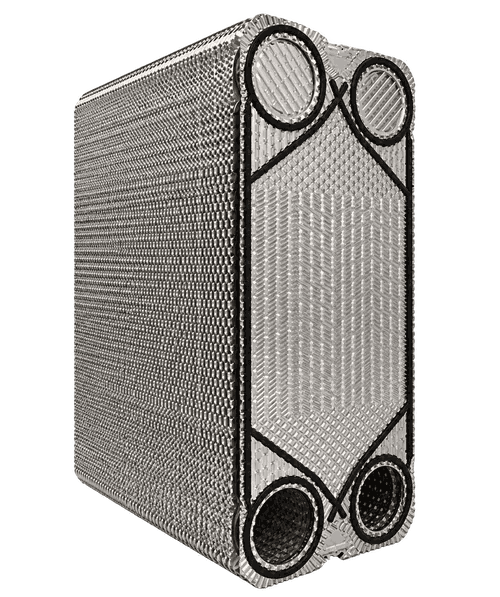
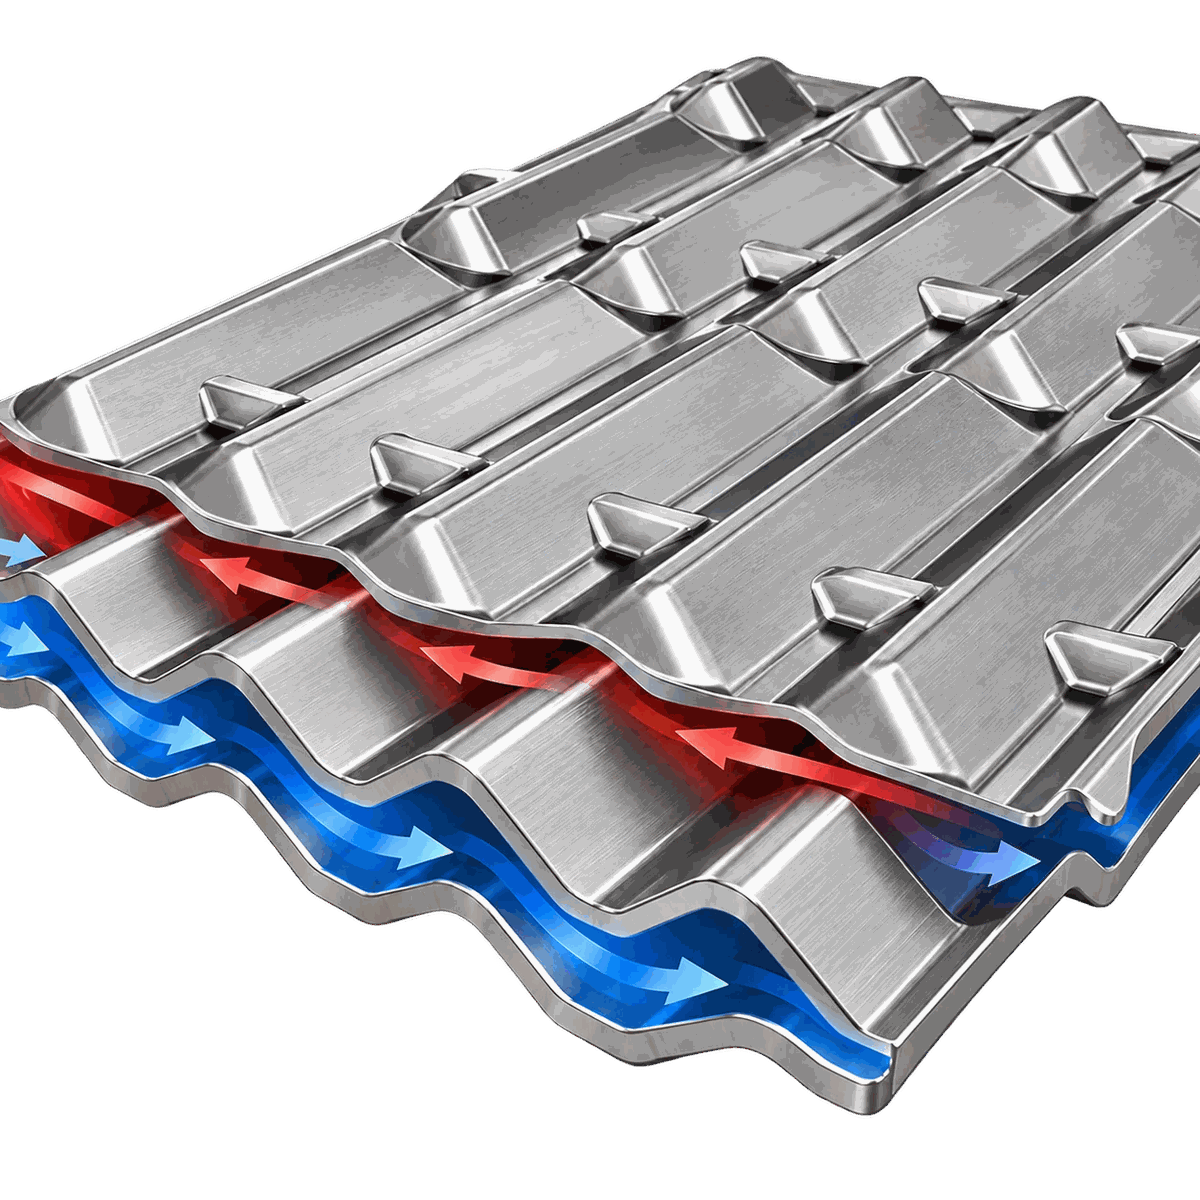
Talk to an Application SpecialistA plate pack reaches a 2 or 3 F approach in true counterflow and recovers 85 to 90 percent of the pasteurizer's heat in regeneration.
Gaskets set the working limit: 250 F for EPDM, 150 psig typical.
Getting a sanitary plate exchanger right
Regeneration is the reason plates win
In a pasteurizer the raw product entering cold and the pasteurized product leaving hot can exchange heat with each other before any steam or chilled water is spent. A plate frame does this in a regeneration section, and 85 to 90 percent regeneration is routine on milk and juice, meaning nine-tenths of the heating and cooling energy is recovered. A shell and tube would need several shells in series to approach the same temperature cross. When the duty has a regeneration section, plates are almost always the answer; the shell and tube then takes the final heating with steam or the cold-side trim if those need higher pressure.
Plate pattern and channel gap set the product limits
Standard chevron plates run a channel gap in the range of 0.1" to 0.15", which is what produces their high coefficients and also what limits them. Water-like product with no solids runs freely. As viscosity climbs past a few hundred centipoise the pressure drop through those narrow channels rises faster than the heat transfer benefit, and by roughly 500 cP the plate is no longer the economical choice. Particulates larger than the gap will lodge at the contact points between plates. Free-flow and wide-gap pressings open the channel to roughly twice the normal gap and pass pulp, fiber and soft particulates up to about 3/8"; beyond that the duty belongs on the tube-in-tube page.
Plate sizing therefore starts from the product's viscosity at the cold end and its largest particle, then works back to the pattern and the number of channels. Sizing from flow and temperature alone is the common mistake and shows up as a pack that plugs in week two.
- Chevron plates: water-like product, highest coefficients
- Free-flow plates: light pulp and small particulates
- Wide-gap plates: about 2x gap, pulp and fibers to 3/8"
- Viscosity above roughly 500 cP: consider tube-in-tube
Gaskets are the working limit
Everything a plate exchanger can survive is set by its gaskets. EPDM handles hot water, CIP caustic and acid, and steam only at low pressure; it is the default for food and dairy. Nitrile covers fats and oils. FKM extends the temperature range and resists more aggressive chemistry at higher cost. All are supplied as food-grade compounds with FDA and 3-A material conformance, and the ports carry a vented double gasket so a failed seal leaks to atmosphere rather than to the other fluid. Plan on gasket replacement as a maintenance item; how often depends on temperature and CIP chemistry, with several years being typical in HTST service.
Opening, inspecting and growing the pack
Loosen the tie bolts, slide the movable frame plate back along the carrying bar, and every plate hangs free for visual inspection of both product and utility surfaces. That is a strong argument for plates in plants whose QA program wants to see the heat transfer surface periodically. The same open frame accepts more plates later: frames are ordered with spare bar length so a duty increase means adding plates and re-tightening rather than replacing the unit.
A plate frame sized for the product's viscosity and solids, gasketed for its temperature and chemistry, and framed with room to grow will carry a pasteurizer for decades.
Call and talk it through with an engineer: 1-805-484-2992
What Buyers Ask First
Gasketed chevron for clean, water-like product; double-wall where the utility must never reach product; wide-gap where pulp or soft solids would lodge. Decide in that order. If the utility is inhibited glycol, tower water or plant condensate against a product with no kill step downstream, the double-wall plate pays for its 10 to 20 percent extra area. If the product carries pulp, trub or fiber, the wide-gap pressing keeps the pack open. One frame can combine them: wide-gap heating and regeneration sections on a juice pasteurizer feeding a double-wall glycol cooler at the end.
About nine-tenths of it: at 90 percent regeneration a 100 gpm milk heater buys roughly 600,000 Btu/h of steam instead of 6 million. The arithmetic, using the water rule of 500 Btu/h per gpm per F, which is close enough for milk, is 100 gpm times 500 times the 121 F rise from 40 to 161 F, which is 6,050,000 Btu/h of heating. Regeneration supplies 90 percent of that from the pasteurized product on its way to the cooler, leaving about 605,000 Btu/h for the hot water section, and the cooler shrinks by the same share. At roughly 900 Btu per pound of plant steam that is the difference between 6,700 and 670 lb/h. The saving is why a plate frame is chosen even when a shell and tube would do the thermal job.
The distance between the fixed and movable frame plates when the pack is correctly compressed, stated on the data sheet for each plate count. Closing past the minimum crushes the gaskets and can crack plates at the contact points; stopping short leaves gaskets unseated and the pack weeps at the first thermal cycle. The figure changes whenever plates are added or gaskets are replaced, so ask for both the nominal and minimum dimension on the data sheet and record the actual measurement after every closing.
Flows, inlet and outlet temperatures on every section, viscosity at the coldest point, largest particle, the regeneration percentage wanted, and the pump head and CIP flow available. The first four decide plate pattern and whether plates fit at all; the last three decide how many plates and whether the pack can be cleaned. On an HTST frame also state the hold temperature and the pressure differential the regulator requires across regeneration, since the booster pump and plate count are sized together. Leaving out the CIP flow is the common gap, and it produces a pack that meets the duty and fails the swab.
Pick the plate size from the flow, not the area; port velocity and channel count decide it. Plates run from 0.5 to 51 sq ft each, and for a given flow a larger plate puts the same gpm through fewer, longer channels at a larger port. Too small a plate means a 6 inch port on a tall stack of tiny channels and a frame as long as a car; too large means a dozen channels running slow, below the velocity that keeps them clean. The sizing software lands on a plate whose port carries the flow at a sensible velocity and whose channel count gives 1.5 times product velocity in CIP.
Because condensing steam puts the plate wall near steam temperature, which bakes protein and sugar onto the product side and shortens gasket life. Even 5 psig steam condenses at 227 F against milk being heated to 161 F, a wall more than 60 F above the product where the film burns on. A hot water set, a closed loop heated by steam through an injector or a small shell and tube, holds the water 3 to 5 F above the outlet temperature, so the wall is barely hotter than the product. The gaskets see about 165 F instead of 227 F, burn-on drops, and the hold temperature controls more smoothly because the water loop damps steam pressure swings.
Related
Sanitary Exchangers
Shell & Tube
Straight tube, U-tube and double tubesheet bundles built for steam, pressure and a clean CIP return.
+ Learn More
Sanitary Exchangers
Tube-in-Tube
One straight product tube inside a jacket: nothing to plug, nothing to bridge, and full counterflow.
+ Learn More
Sanitary Exchangers
Embossed Plate
Two stainless sheets welded and inflated into a heat transfer surface that goes wherever the tank needs it.
+ Learn More